
 EN
Cutting room supervisors know the number that rarely makes it onto a sustainability dashboard: fabric lost as offcuts during spreading and cutting. Industry studies put that figure around 15% in conventional cutting rooms, and it sits alongside a larger pattern. The global textile industry generates an estimated 92 to 110 million tons of waste annually, with 25% to 40% of fabric used in garment production becoming pre-consumer waste before a finished product ever ships. A good portion of that loss is not design-driven. It happens because a cut edge frays, a panel gets rejected, or a sealing step downstream consumes extra material to make an edge behave.
Ultrasonic cutting changes the math at the point where the cut is made. Instead of slicing fibers and leaving a raw edge for a later process to stabilize, a vibrating blade melts and fuses thermoplastic fibers along the cut line. The fabric separates cleanly and the edge is sealed in the same motion. That single change removes a category of waste that conventional cutting rooms treat as unavoidable.
Where fabric waste actually hides in a cutting room
Most waste conversations focus on the marker and the nesting software. Better nesting absolutely matters, and optimized layouts can recover meaningful percentage points of fabric utilization. But nesting only decides where the blade travels. It does not control what happens to the edge after the blade passes through.
A woven synthetic fabric cut with a mechanical knife leaves loose yarn ends. Those ends ravel during handling, during stacking, and during transport to the sewing floor. Panels that ravel at the edge get trimmed again, rejected, or sewn with a wider seam allowance to bury the mess. Each of those responses consumes fabric that the marker said was already saved. The waste is invisible on the cut plan but very visible in the scrap bin.
Heat-sealed edges close that loop. When the cut edge is fused, there is no loose yarn to ravel. Panels stack flatter, handle faster, and arrive at the next station with a dimensionally stable boundary. The saving is not just the offcut. It is the rework and the oversized seam allowance that never has to be added in the first place.
The mechanics behind a sealed edge
An ultrasonic cutting head operates in the 20 kHz to 40 kHz range. The blade vibrates at high frequency with low amplitude, and when it contacts the fabric against an anvil, the vibration energy is converted into localized heat at the interface. Thermoplastic fibers, meaning polyester, nylon, polypropylene, and similar synthetics, melt at that narrow zone and resolidify as a fused edge as the blade advances.
The cut is not a sawing action. The tool essentially parts the material while welding the boundary shut. That distinction matters because it eliminates the need for a separate hemming, binding, or overlocking pass on edges where a turned hem is not required or not acceptable. For curtain panels, filter media, automotive interior textiles, and industrial fabrics, the sealed edge is often the finished edge.
There is a practical side benefit in the cutting room. A fused edge is dimensionally locked. It will not grow a fringe of loose threads that changes the panel’s effective size after cutting. The cut part that leaves the table is the part that arrives at assembly, which makes downstream planning more predictable.
A three-way comparison of edge outcomes
The table below summarizes the edge condition and material fit for the three cutting approaches most commonly found in fabric processing. It is not a ranking of machines. It is a map of what each method does to the boundary of the part.
| Cutting method | Edge condition after cut | Fraying risk | Best-fit materials | Heat-affected zone |
|---|---|---|---|---|
| Mechanical blade | Raw, loose fibers at the cut line | High on woven synthetics and blends | Natural fibers, very thick stacks, low-melt-sensitive goods | None |
| Laser | Sealed but often charred or discolored | Low | Thin synthetics where edge appearance is secondary | Wide, with odor and fume extraction required |
| Ultrasonic | Fused and clean, no loose fiber | Low on thermoplastic content | Synthetics, blends, nonwovens, coated textiles | Narrow, localized at the cut interface |
The laser column is where a lot of shops get surprised. Laser cutting seals the edge, but the thermal load is broad and the charring can make a white or light-colored fabric unusable at the boundary. Ultrasonic cutting concentrates the heat into a much tighter zone, so the edge seals without cooking the surrounding material.
What ultrasonic cutting will not fix
Honest conversations about any cutting technology have to include the materials it struggles with. Ultrasonic sealing depends on a thermoplastic component in the fabric. Pure cotton, wool, linen, and other natural fibers without a synthetic blend do not melt and fuse the same way. They may cut, but the edge will not seal, and the fraying advantage disappears.
Thickness and stack height also impose limits. Very thick multi-layer stacks or heavily reinforced composites can exceed the power and amplitude available from a given cutting head. In those cases the tool may bond layers rather than sever them cleanly, or the cut speed has to drop to a point that changes the production math. Ultrasonic cutting is not a universal replacement for every knife in the building. It is a targeted fix for the edge-stability problem on thermoplastic-rich materials.
That limitation is worth stating plainly because it shapes where the technology pays back fastest. A shop cutting mostly polyester curtain fabric or nylon automotive trim will see a different return than a shop cutting heavyweight natural canvas. The material mix decides the fit.
A cutting room change that started with a scrap count
A curtain and drapery manufacturer running three mechanical cutting tables began tracking scrap by cause rather than by total weight. The total scrap number had been stable for months, which made it look like a nesting problem that had already been optimized. The breakdown told a different story. A meaningful share of rejected panels came from edge raveling that occurred after cutting, not from pattern inefficiency on the table.
The first trial replaced one mechanical head with an ultrasonic unit on the polyester and polyester-blend curtain fabrics. The immediate change was in handling. Panels could be stacked and moved without the edge shedding fibers. The second change was less obvious but more important financially: the downstream hemming station no longer had to trim a raveled edge before folding. That trim operation had been consuming both labor and fabric, and it disappeared from the routing for the ultrasonic-cut panels.
The trial did not convert the entire cutting room. The natural-fiber decorative line stayed on mechanical cutting because the edge would not seal. But on the synthetic curtain line, the scrap-by-cause count dropped, and the hemming station’s workload became more predictable. That is the realistic version of an ultrasonic cutting adoption: it wins on a defined material set, not across every SKU in the building.
Where the equipment side makes the difference
The gap between a working ultrasonic cutting installation and a frustrating one usually comes down to the hardware’s ability to hold frequency and amplitude stable across a production shift. A cutting head that drifts in frequency will start leaving partially sealed edges, and a partially sealed edge is worse than a raw edge because it looks finished until the panel is handled. Tooling geometry, anvil flatness, and the control system’s response to material thickness variation all influence whether the sealed edge is consistent from the first meter of fabric to the last.
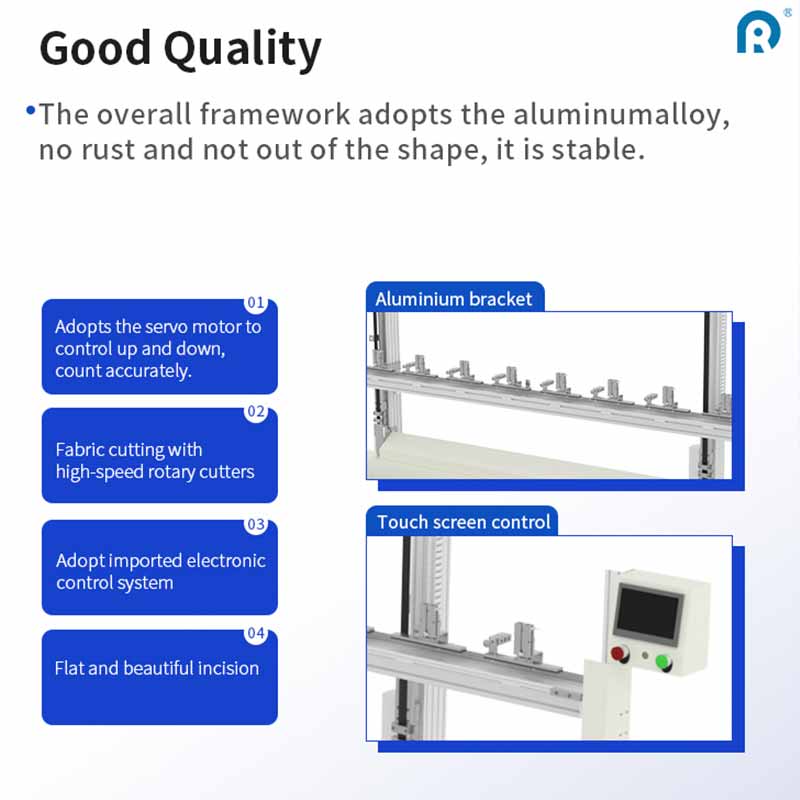
Dongguan Ridong Intelligent Equipment Co., Ltd. builds ultrasonic cutting equipment for fabric and flexible material processing, with a focus on the cutting head, automation integration, and the mechanical stability that keeps edge quality repeatable over long runs. The company’s manufacturing base and quality control processes are set up around the kind of production environment where a cutting room runs multiple shifts and cannot afford edge quality that changes with tool temperature or operator feel. For operations evaluating ultrasonic cutting as a waste-reduction move, the practical question is less about whether the principle works and more about whether the specific machine holds the principle steady across the material mix on the floor.


